In modern manufacturing and material handling operations, reliable transportation of heavy or bulky products is essential for maintaining productivity and operational efficiency. The chain conveyor is a robust and durable solution designed to handle demanding industrial environments where standard belt conveyors may not be sufficient.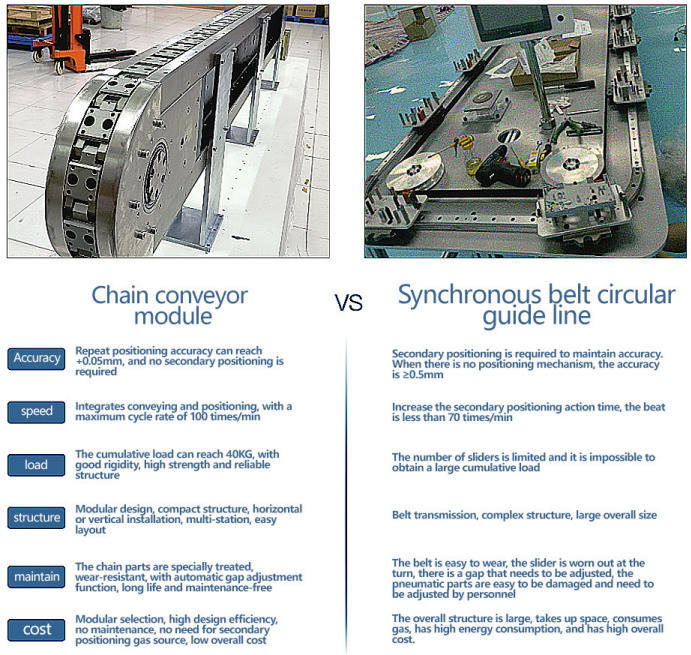
For OEM equipment manufacturers and system integrators, working with experienced suppliers to develop custom chain conveyor systems ensures optimal performance, durability, and seamless integration into production lines.
A chain conveyor is a type of conveyor system that uses chains to move products along a production line. It is specifically designed for applications requiring high load capacity, durability, and resistance to harsh operating conditions.
Typical configurations include:
These systems are widely used in industries where strength and reliability are critical.
Standard conveyor solutions may not meet the specific needs of complex industrial environments. This is why many companies rely on custom chain conveyor manufacturers to design systems tailored to their applications.
Customization options include:
Custom design ensures that the conveyor system operates efficiently under real production conditions.
Chain conveyors are ideal for transporting heavy products such as pallets, automotive parts, and industrial components.
Designed for harsh environments, these systems offer excellent resistance to wear, impact, and extreme conditions.
Chain-driven movement ensures consistent transport even under heavy loads.
Custom configurations allow adaptation to complex production line layouts.
With robust construction, chain conveyors require minimal maintenance compared to other heavy-duty systems.
Industrial chain conveyor systems are widely used in various sectors requiring reliable heavy-duty material handling.
Common applications include:
These applications benefit from the strength and durability of chain conveyor solutions.
Modern chain conveyor systems can be seamlessly integrated into automation environments, including:
This integration enables efficient and synchronized material flow across the entire production process.
When selecting a supplier for custom chain conveyor systems, consider the following factors:
A reliable manufacturer ensures long-term system performance and reduced operational risks.
As industrial automation continues to evolve, the need for robust and efficient material handling systems is growing. The chain conveyor remains a key solution for heavy-duty applications, offering durability, flexibility, and reliable performance.
By partnering with experienced chain conveyor manufacturers, companies can develop customized conveyor systems that meet their exact production requirements and support long-term operational success.