In modern industrial environments, efficiency, consistency, and automation are essential for staying competitive. Manufacturing conveyor systems play a critical role in streamlining production processes by enabling smooth and continuous material flow across different stages of manufacturing.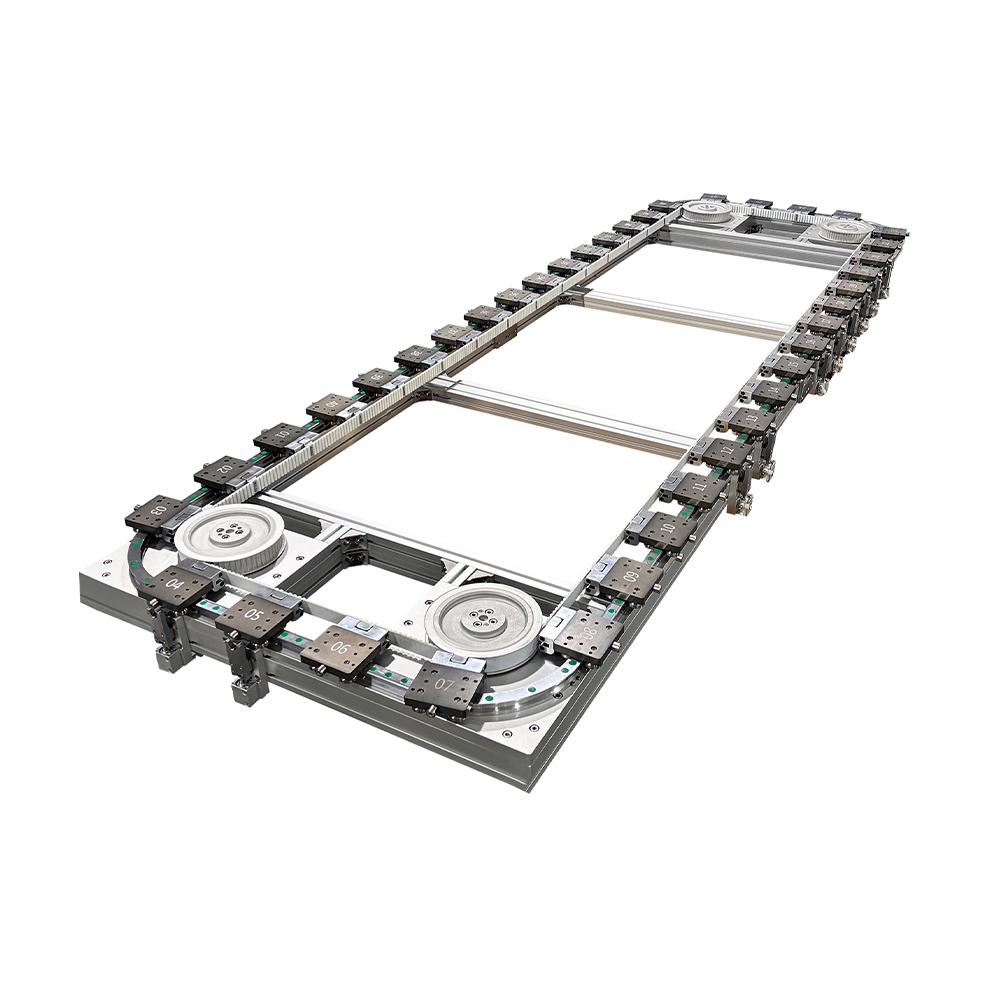
From simple transport tasks to fully automated production lines, conveyor systems are widely used to improve productivity, reduce manual labor, and enhance operational efficiency.
Manufacturing conveyor systems are mechanical handling solutions designed to move materials, components, or finished products within a production facility. These systems can be customized to fit specific workflows, ensuring seamless integration into manufacturing operations.
A typical conveyor system includes:
Together, these elements create a reliable and efficient material handling system.
Different manufacturing processes require different conveyor solutions. Common types include:
Ideal for transporting lightweight to medium-weight products with smooth and continuous movement across long distances.
Designed for heavy-duty applications, capable of handling pallets, large components, and high-load materials.
Used for manual or gravity-driven movement, often found in assembly lines and warehouses.
Flexible systems that can be easily reconfigured to adapt to changing production requirements.
Integrated with sensors, PLCs, and robotics for fully automated material handling and production processes.
Conveyor systems enable continuous material flow, reducing delays and increasing throughput.
Automation minimizes manual handling, allowing workers to focus on higher-value tasks.
By reducing manual lifting and transportation, conveyor systems lower the risk of workplace injuries.
Controlled movement ensures uniform processing and reduces product damage.
Systems can be expanded or modified as production demands grow.
Manufacturing conveyor systems are used across a wide range of industries:
These systems help optimize workflows and improve overall operational performance.
Many factories require tailored solutions to meet specific operational needs. Custom manufacturing conveyor systems offer:
Custom solutions ensure maximum efficiency and seamless integration into existing production lines.
When selecting or designing a manufacturing conveyor system, consider the following factors:
Material type: Size, weight, and fragility of products.
Production speed: Required throughput and cycle time.
Facility layout: Space constraints and system configuration.
Environmental conditions: Temperature, humidity, and cleanliness.
Automation level: Integration with control systems and software.
Careful planning ensures optimal performance and long-term reliability.
A reliable conveyor system manufacturer is essential for successful implementation. Look for a partner that provides:
Working with an experienced supplier ensures your system meets both current and future production needs.
As industries continue to adopt automation and smart manufacturing, manufacturing conveyor systems have become indispensable for efficient production. They provide reliable, scalable, and cost-effective solutions for material handling across various industries.
Whether you need a standard system or a fully customized solution, investing in the right conveyor system can significantly improve productivity, reduce costs, and enhance overall operational efficiency.